1. Project Name
UK Smart Factory Deployment: Indoor Cabinet Air Conditioners for PLC & Servo Drive Enclosures
2. Client Background
Our client is a leading industrial automation systems integrator based in the United Kingdom, specializing in smart manufacturing and fully automated production lines. Their end-user is a large-scale automotive parts manufacturer with a new smart factory in England. The cooling units are installed on PLC control cabinets and servo drive cabinets distributed across the workshop floor, where ambient temperatures can reach 40°c due to adjacent furnaces and process heat.
3. Project Requirements and Challenges
The client set four critical requirements:
IP54 protection - Cabinets must be safeguarded against dust ingress and water splashes common in industrial environments (coolant mist, wash-down residues).
Remote monitoring & predictive maintenance - The cooling system must support RS485 Modbus communication for integration with the factory’s central SCADA, enabling real-time alerts on temperature deviations and compressor health.
Built-in condensate evaporator - To eliminate manual drainage and floor puddles, the units must automatically evaporate all internal condensate into the hot exhaust air.
Aesthetic design - The cabinets are visible to clients during factory tours, so the cooling units need a sleek, compact appearance that aligns with the facility’s modern industrial branding.
4. Our Solution
We recommended a customized four-model lineup of air-cooled cabinet air conditioners, tailored to varying heat loads across different cabinet sizes:
CTACG0326NEP 300 W Small PLC I/O cabinets
CTACG0826NEP 800 W Medium PLC racks & power supplies
CTACG2026NEP 2,000 W Large servo drive cabinets
CTACG2526NEP 2,500 W High-density drive clusters
All models feature:
High-efficiency rotary compressor for energy savings.
IP54-rated housing with powder-coated steel (RAL 7035) - aesthetically neutral and scratch-resistant.
Built-in condensate evaporator - utilizing hot discharge air to vaporize moisture, achieving 100% drainage-free operation.
Standard RS485 communication module - supporting Modbus RTU, transmitting supply/return air temperatures, compressor run time, fan speed, and 8 fault codes.
Compact design to maintain a clean, flush-mounted look on cabinet doors.
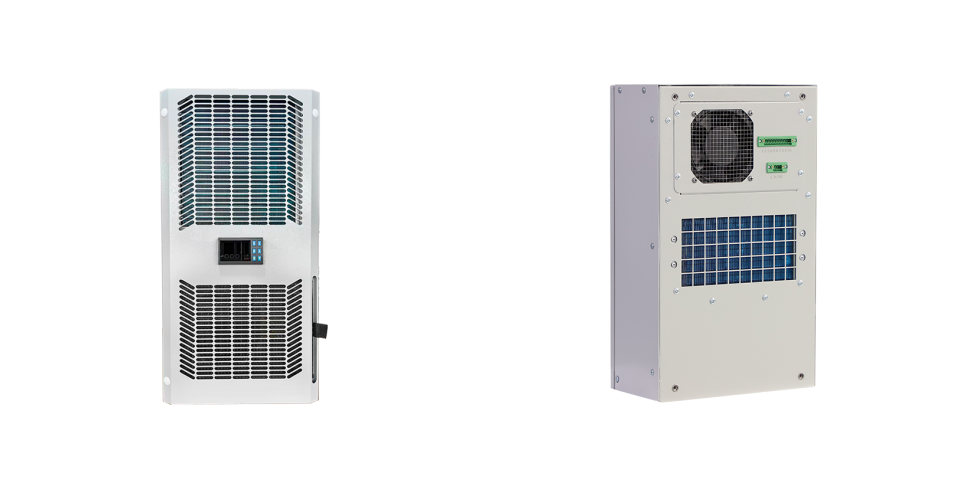
CTACG0826WNEP
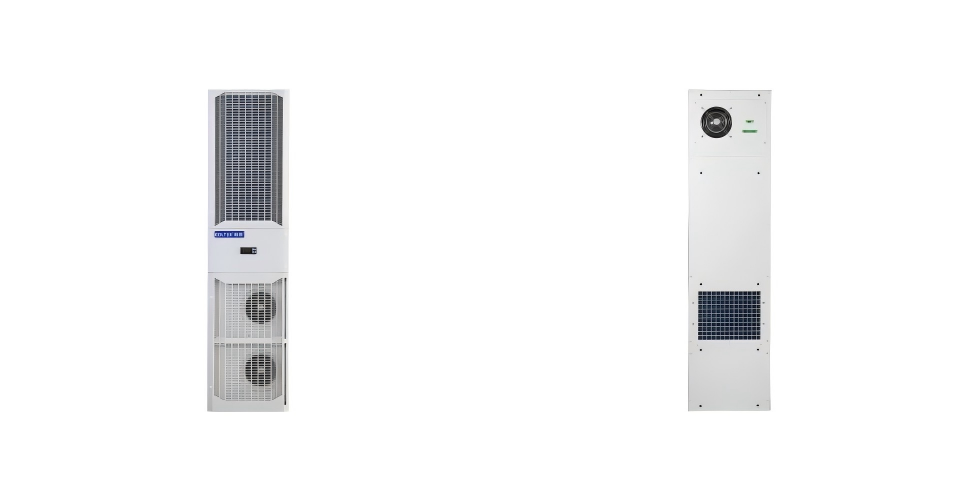
CTACG2026WNEP
5. Installation and Deployment Process
Delivery - 16 pilot units (various models) were delivered via sea freight .
Installation - Each unit quick-connect power terminals. Local electricians completed installation within a short period. The RS485 daisy-chain wiring was integrated alongside the cabinet’s existing fieldbus network.
6. Project Outcomes and Client Feedback
After days of continuous operation, all cabinet air conditioners maintained internal temperatures between 30-35°C, even during peak workshop heat. The condensate evaporator eliminated all drip-tray maintenance - a significant labor saving. The client’s maintenance manager reported: “We’ve reduced unscheduled downtime by over 70% compared to our previous fan-only cooling method. The management has decided to reorder another 20 units.”